Short answer
A hot bed, even heat around the print and moderate speed. The nozzle temperature matters less than keeping the part warm all the way through, so the corners don't lift.
How to print ABS: quick guide
ABS gives tough, heat-resistant parts but is trickier than PLA and PETG, because the corners tend to lift (warping). To read up on the material itself, see What is ABS? This guide goes straight to getting even, reliable prints with the right temperatures and a stable environment. All temperatures below come from our own data sheets.
Recommended settings
Starting values according to our data sheets. Of everything here, it is the heated bed and a stable environment that decide whether the print succeeds or not.
Step by step
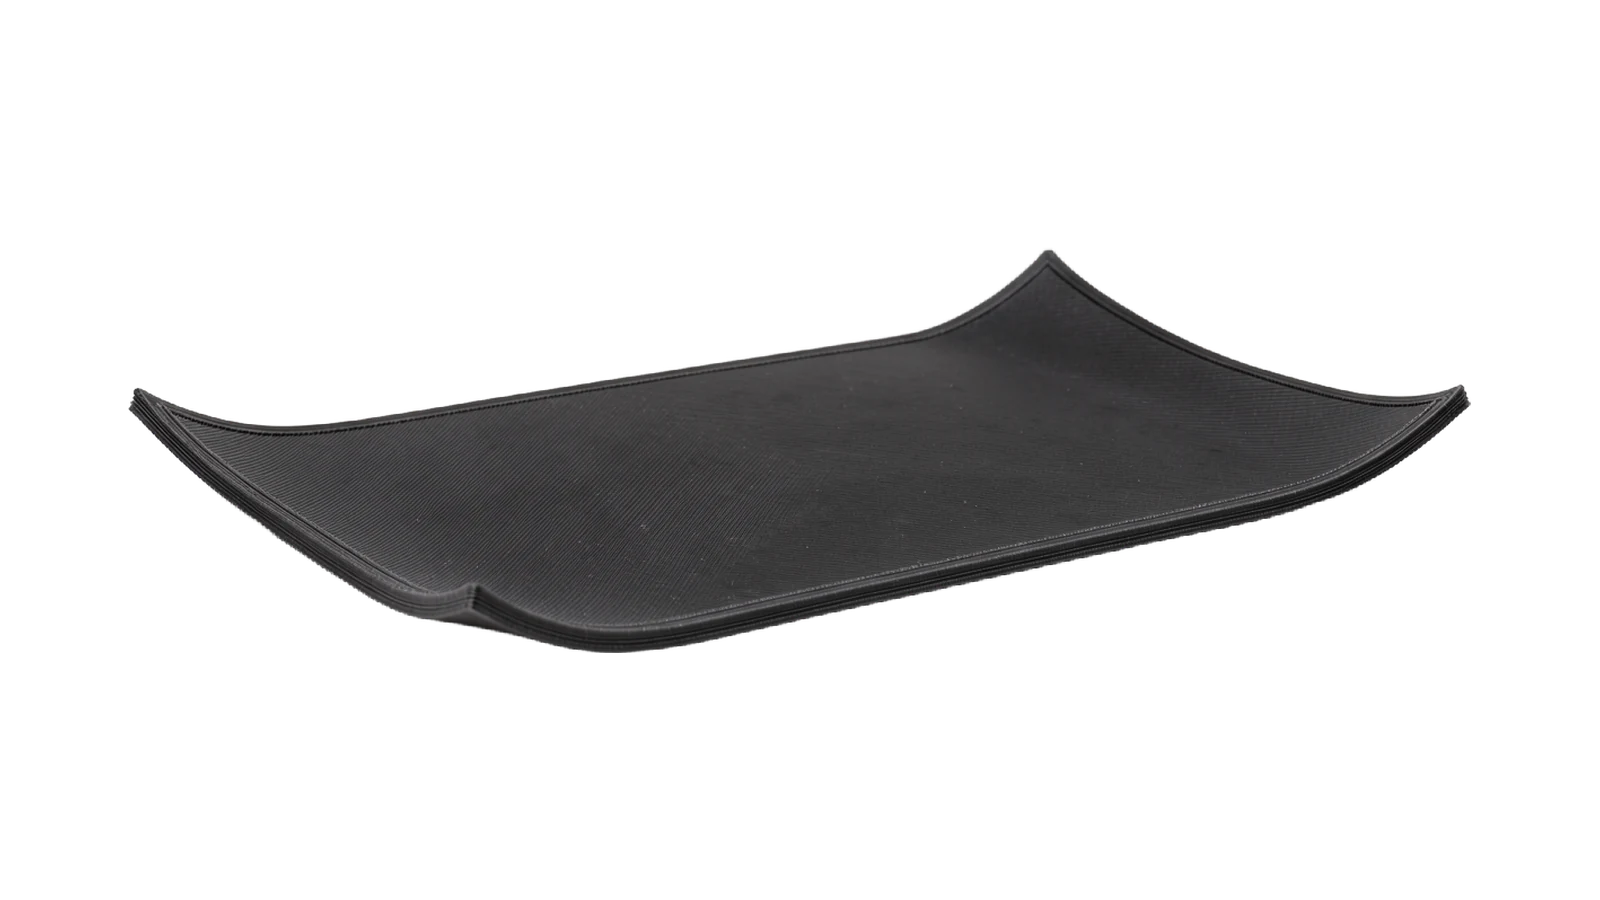
1. Create a stable, warm environment. ABS shrinks as it cools, and uneven cooling is what makes the corners lift off the bed. The easiest fix is to print in an enclosed printer or an enclosure that keeps the heat even, and to avoid cold, draughty rooms. Keep the room at 20 °C or more. If the corners still lift, there are more tips in the warping guide. Remember ventilation, as ABS smells while printing.
2. Make the part stick. The foundation is a heated bed, 90–110 °C. If you want extra grip, especially on larger parts, reach for a glue stick or a brim around the model. A PEI plate or similar surface also helps. And consider raising the bed and nozzle temperature by 5–10 °C for the first layer only.
3. Keep cooling down. This is where ABS differs a lot from PLA: the less layer cooling, the better. If the layers cool too quickly they bond less well, and the risk of warping and cracking goes up. Turn the fan off or run it at the lowest setting.
Common problems and solutions
Good to know
→ With an enclosure
An enclosed printer makes ABS far more reliable. The heat stays even, there is less warping, and even large parts come out strong and dimensionally stable.
→ Without an enclosure
You can print smaller ABS parts without an enclosure if the room is warm and free of draughts. Use a brim, a hot bed and no layer cooling. Expect corners on large surfaces to lift more easily.
Frequently asked questions about printing ABS
What temperature should I print ABS at?
230–260 °C on the nozzle and 90–110 °C on the bed, according to our data sheets. Run the nozzle at 245 °C and the bed as hot as your printer allows. The bed temperature is what protects against warping.
Why do the corners of my ABS print lift?
It shrinks as it cools, and uneven cooling makes the corners lift. The solution: an even, warm environment. Enclosed printer, raised bed temperature, no draughts. A brim and glue stick help at the margin.
Do I need an enclosed printer for ABS?
Not strictly required for smaller parts, but strongly recommended. An enclosure keeps the heat even and means much less warping and cracking. Make sure ventilation is good.
Should I have layer cooling on for ABS?
No. Keep it as low as possible, ideally off. ABS bonds best between layers without cooling. Too much fan raises the risk of both delamination and warping.
ABS in 23+ shades, from 125 SEK
Every colour test-printed, vacuum-packed with a silica gel sachet and shipped from Tibro within 48 hours.