Short answer
Clean the bed with dish soap, level it, and check that the first layer is pressed out into an even, smooth line. If that does not solve it, the temperature or speed needs adjusting.
Print not sticking: the short answer
A first layer that does not stick is the most common problem in 3D printing, and it almost always has one of three causes: the wrong distance between nozzle and bed, a dirty build plate or the wrong bed temperature. All three can be fixed in a few minutes, and this guide takes them in turn.
Rule of thumb: Clean the bed with dish soap, level it, and check that the first layer is pressed out into an even, smooth line. If that does not solve it, the temperature or speed needs adjusting.
Find the cause step by step
1. Clean the build plate. Grease from fingers is the single most common culprit. Wash the plate with warm water and dish soap, dry it with a clean cloth and then avoid touching the surface. Isopropanol works for quick cleaning between prints, but dish soap removes grease better. This is a general tip that applies to all materials.
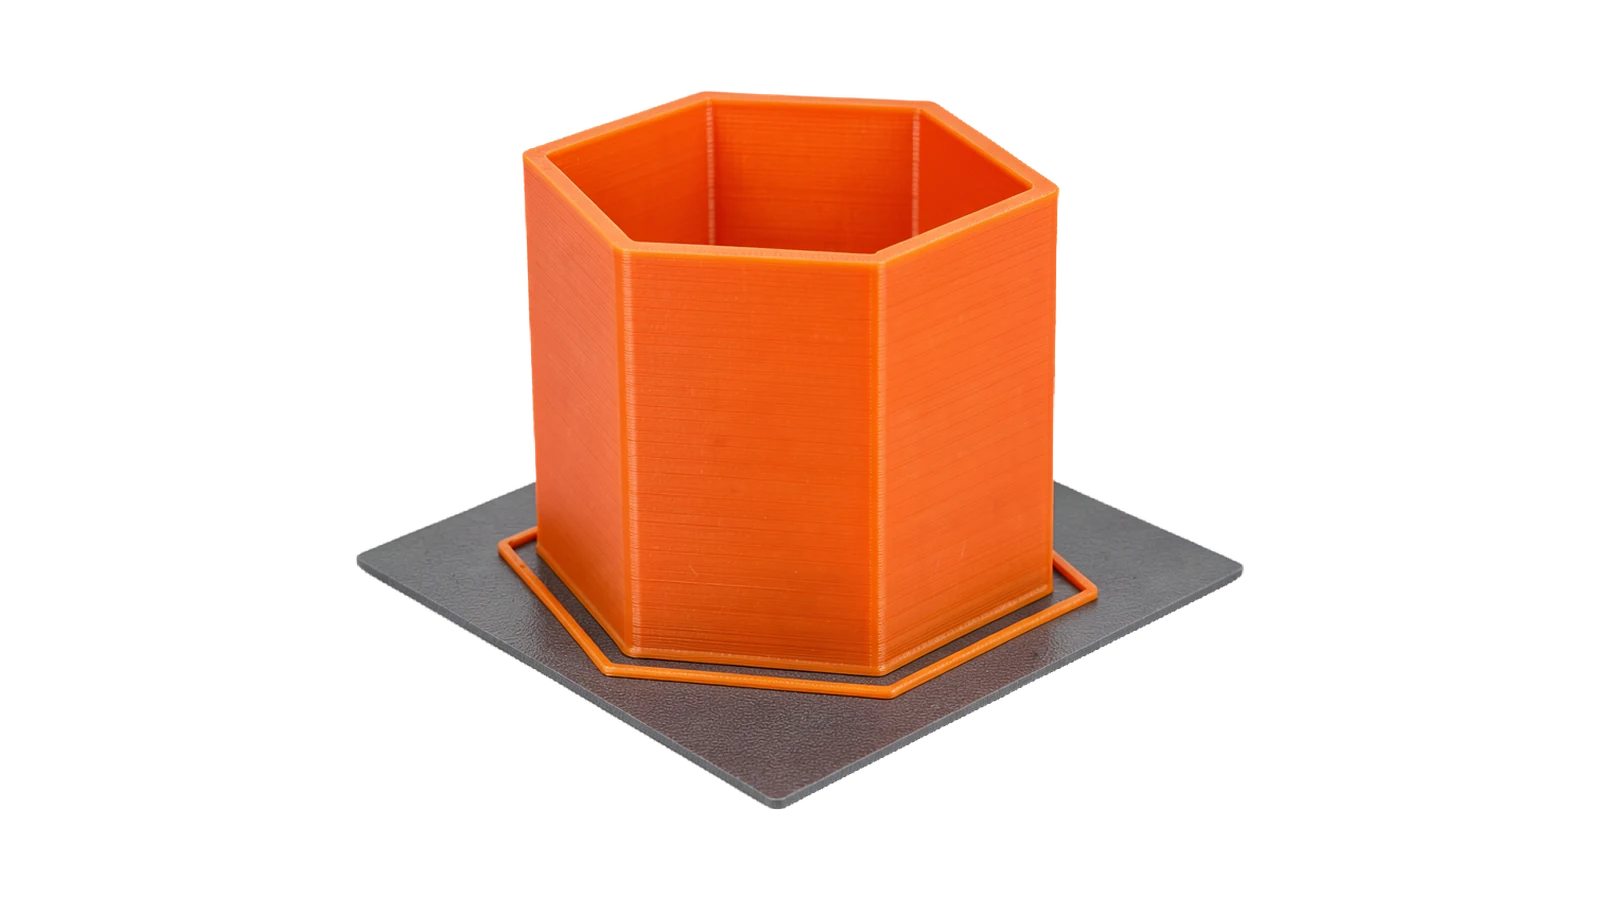
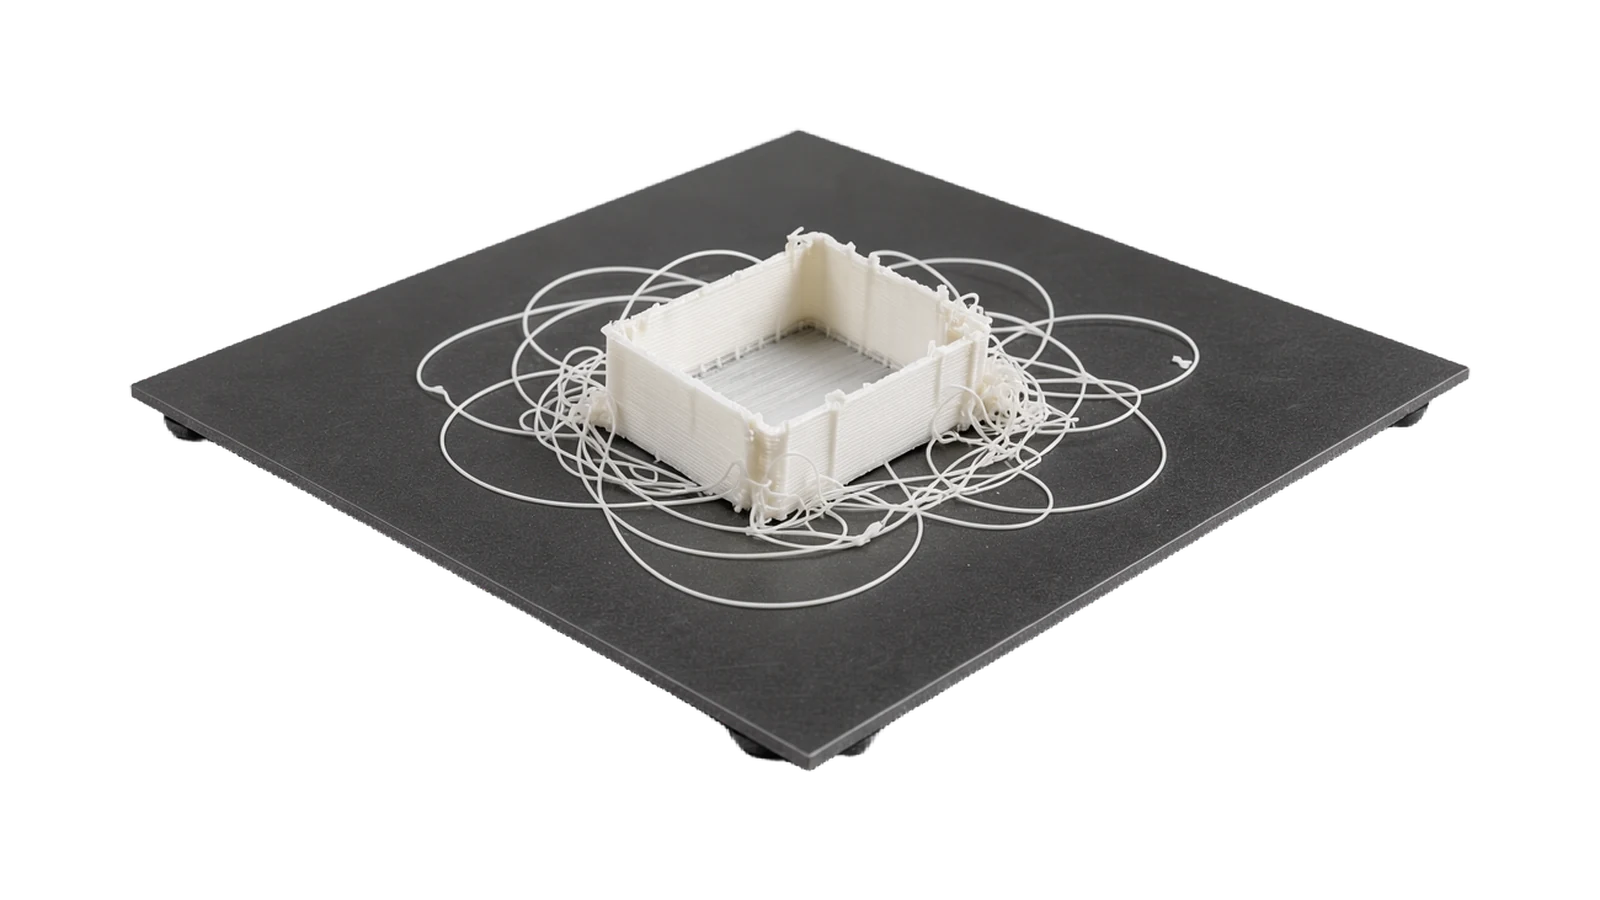
2. Set the distance to the bed. The nozzle should be close enough that the filament strand is pressed lightly against the plate. If the strand just lies loosely on top, the gap is too big. Level the bed and fine-tune with z-offset: if the first layer looks like round, loose spaghetti strands the nozzle is too high, and if it comes out see-through thin and uneven it is too low. Materials also behave differently: PLA likes to be pressed against the surface, while PETG wants a little more room. We cover this in How to print PLA and How to print PETG.
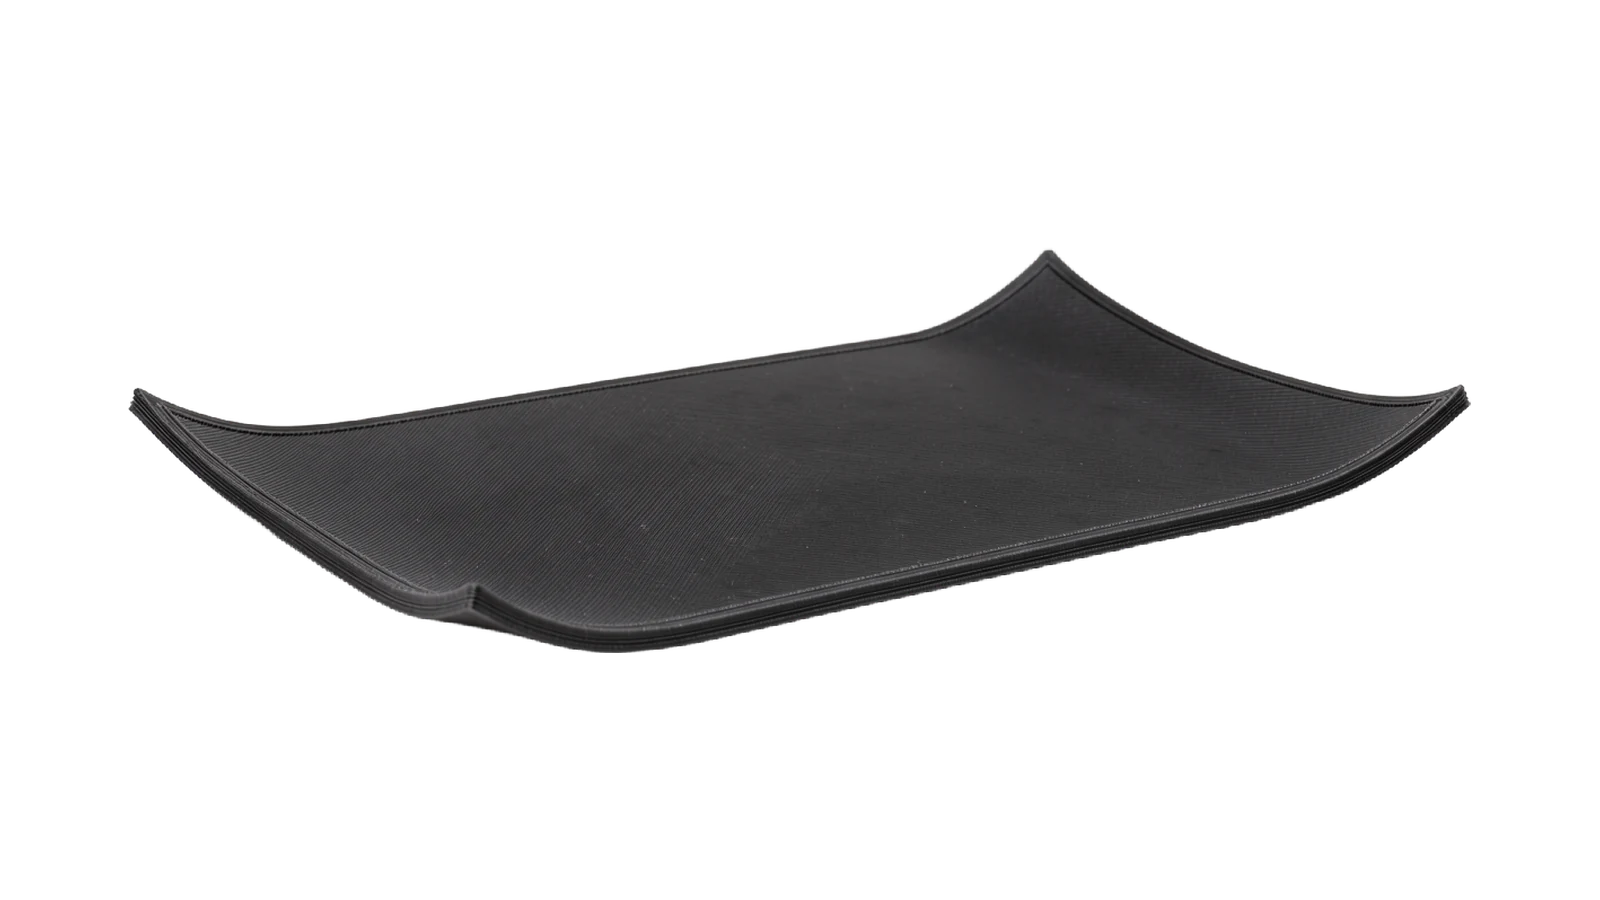
3. Check the bed temperature. At the wrong bed temperature, even a good first layer lets go after a few minutes. Our data sheets give 40–65 °C for PLA, 50–70 °C for PETG and 90–110 °C for ABS and ASA. ABS is especially sensitive: a bed that is too cool is the most common reason the corners lift. There is more on that in the guide on warping.
4. Lower the first-layer speed. A first layer printed too fast does not have time to stick. Reduce the first-layer speed to roughly half of the normal speed in your slicer. Most slicers have a separate setting for the first layer.
Settings by material
The table summarises the bed temperatures from our data sheets and what each material wants beyond that.
When nothing else helps
If it still won't stick, there are two proven tricks. A glue stick on the plate gives extra grip for almost any material and washes off easily. A brim, a wide edge around the model that the slicer adds, increases the contact area a lot and helps narrow, tall parts in particular. If the filament is old and has been left out, moisture can also weaken adhesion. You will find more signs of that in the guide to drying damp filament.
If you are new to this and want to avoid the problem altogether, PLA filament is the easiest material to get right. It sticks readily to most build plates without a glue stick or a high bed temperature.
Frequently asked questions about bed adhesion
Why won't my PLA stick?
Almost always a dirty plate or the wrong Z distance. Wash the plate with dish soap, level it and make sure the first layer is pressed into an even line. PLA is the material that sticks most easily, so the basics are usually enough.
Do I need a glue stick?
Not for everyday prints in PLA or PETG on a clean plate. A glue stick is, however, a good aid for ABS, ASA and nylon, for large parts with a small contact area, and as a release agent when PETG sticks too hard.
Which build plate surface is best?
A textured PEI plate is a reliable all-round choice that most materials stick to well. Smooth PEI gives a glossier underside but needs more careful cleaning. Cleaning matters more than which surface you pick.
The print comes loose mid-print, why?
If the first layer looked good but the part comes loose later, it is usually due to draughts or a bed that is too cool, so the part shrinks and pries itself free. It is the same mechanism as warping and is covered in that guide.
Filament in 173+ shades, from 113 SEK
Every colour test-printed, vacuum-packed with a silica gel sachet and shipped from Tibro within 48 hours.