Short answer
Start in the middle of the temperature range, keep the speed down for good-looking parts, and make sure the filament is dry. Then PETG prints easily and cleanly.
How to print PETG: quick guide
PETG gives you strong, tough parts with good layer adhesion, but it takes a bit more care than PLA. If you want to read up on the material itself first, we cover it in What is PETG? This guide goes from temperatures to the first layer and the most common problems. All temperatures come from our own data sheets.
Recommended settings
Starting values for PETG according to our data sheets. Exact values vary between printers, colours and variants, so treat them as a starting point to fine-tune from.
Step by step
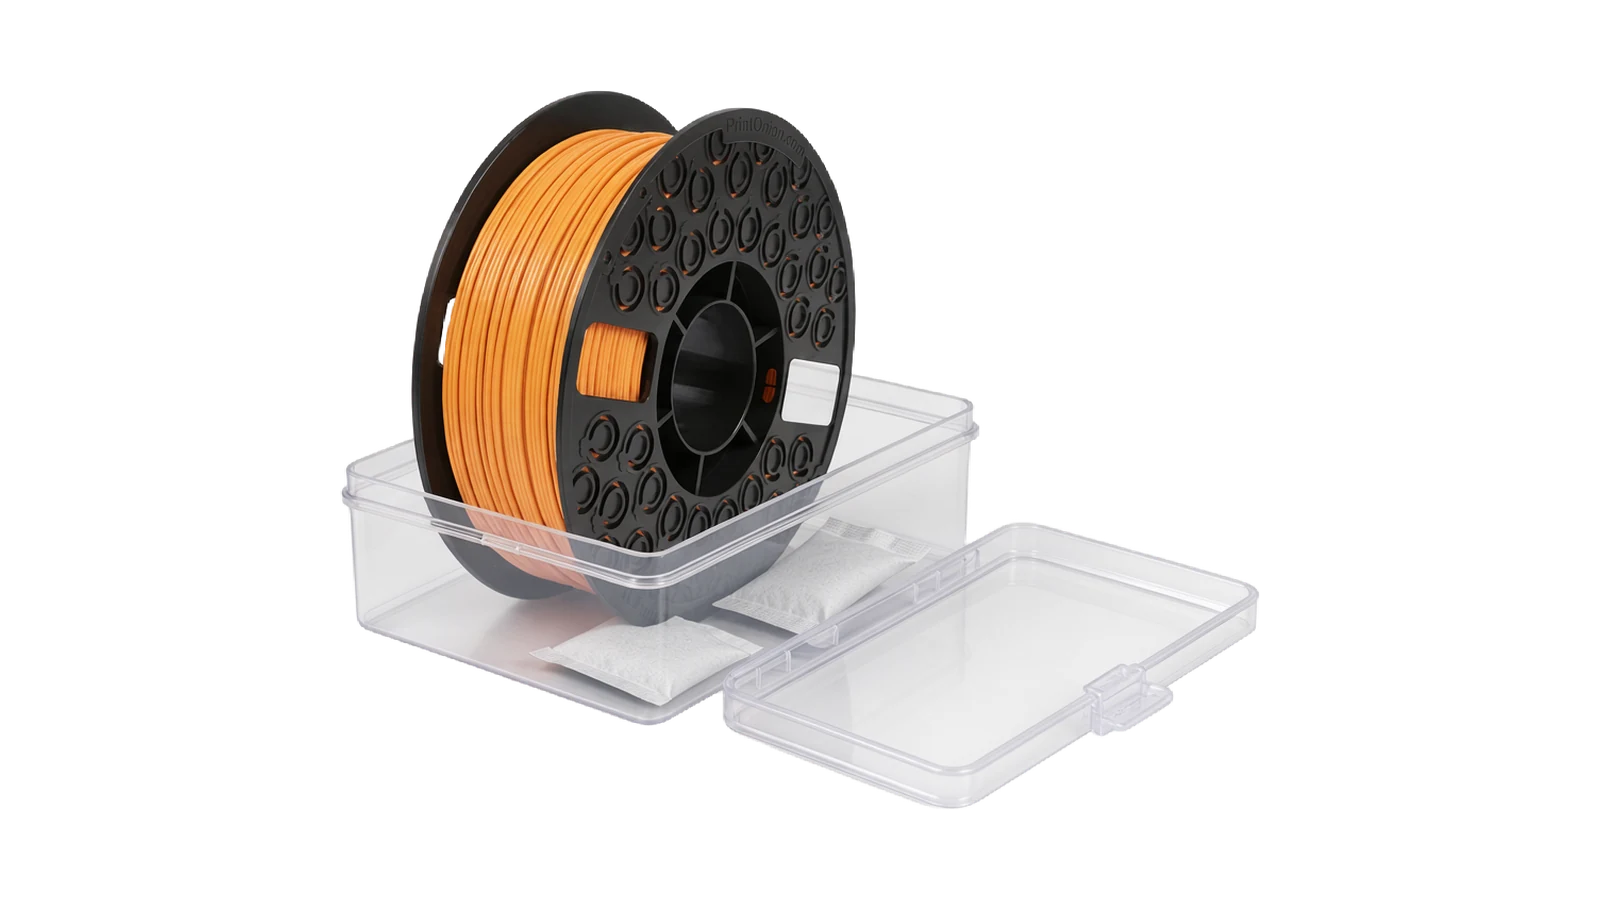
1. Keep the filament dry. PETG is hygroscopic, which means it absorbs moisture from the air. Damp filament gives poorer layer adhesion, brittle parts and more stringing. Store the spool in a resealable bag with desiccant between prints. If you suspect moisture, you can dry the filament in a filament dryer or an oven on low heat before printing. The full routine is in How to dry filament.
2. Get the first layer right. A good first layer is half the job. PETG wants a little more distance between nozzle and bed than PLA, and we go through the differences between the materials in PLA vs PETG. If you press the nozzle too close, it builds up residue that causes blobs, so aim for an even, smooth first line without the strands being squashed together. PETG adheres well to most build plates. If you need extra adhesion on large parts, glue stick or a PEI plate works well.
3. Fine-tune the temperature with a temp tower. The right nozzle temperature is a trade-off between strength and appearance. A lower temperature usually gives less stringing and neater details, while a higher temperature gives stronger layers. A simple way to find the right one is to print a temp tower, a model that is printed in several temperature steps, and pick the step that looks best. This is a general trick that works for all materials.
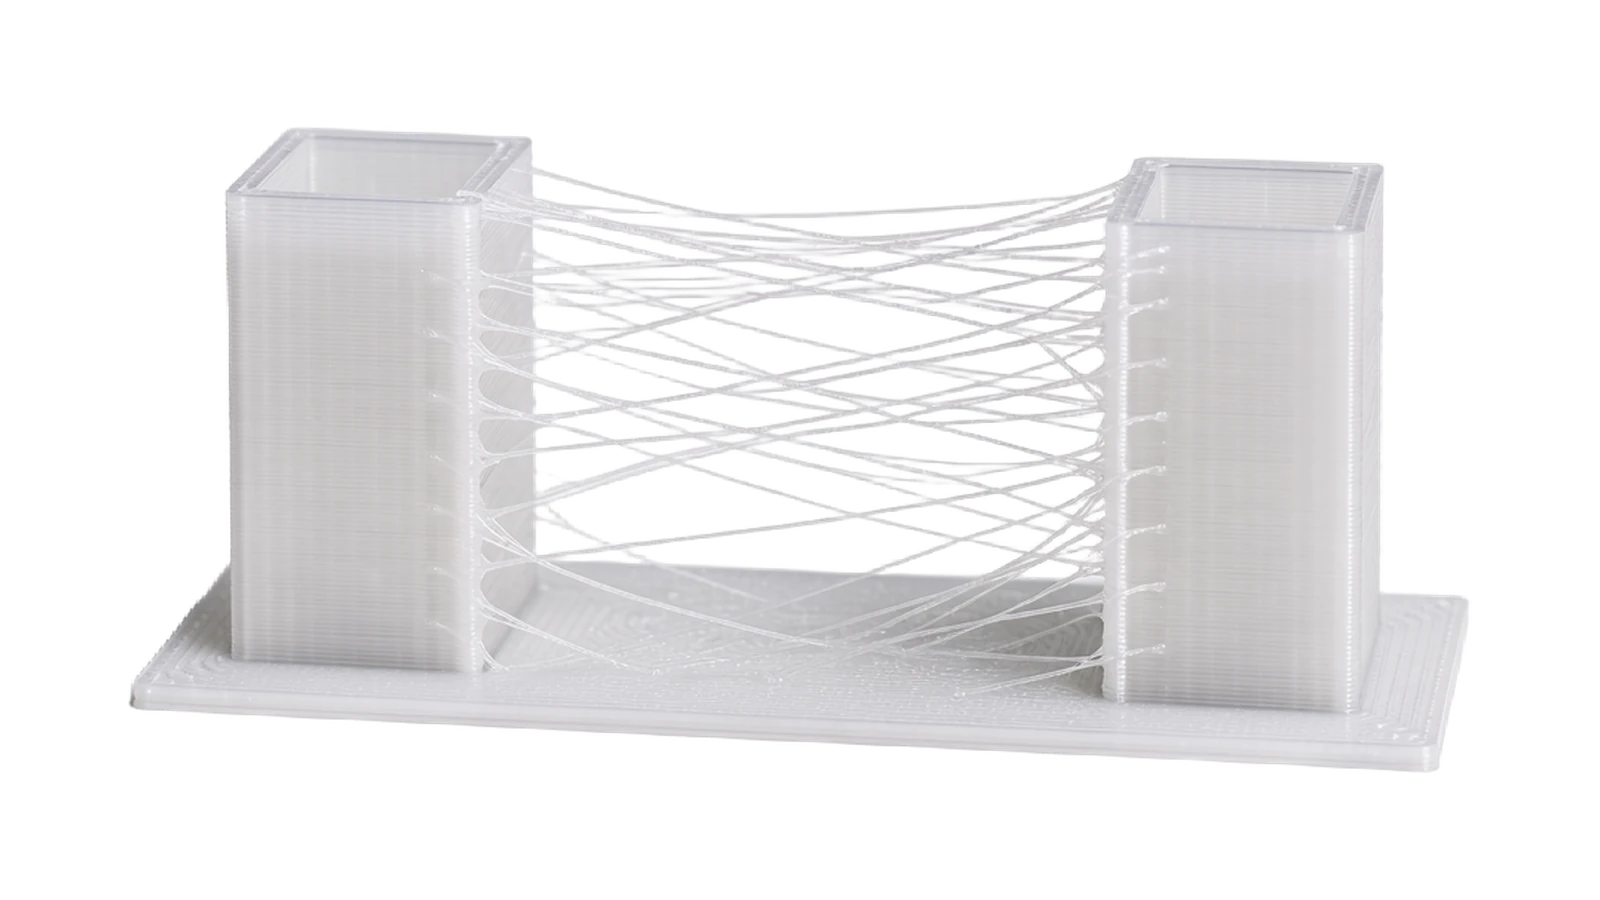
4. Tune retraction against stringing. The most common PETG problems are stringing (thin threads between parts) and blobs. Both are linked to temperature, moisture and retraction settings. Lower the temperature in steps of 5 °C and adjust the retraction distance and speed if you see threads. The "z-hop while retracted" setting can reduce the risk of the nozzle dragging residue along with it. More troubleshooting can be found in the guide to stringing.
Common problems and solutions
Do you want stronger or better-looking parts?
→ Best-looking results
Lower the speed (preferably below 50 mm/s) and the layer height (0.15 mm), and set up retraction carefully. A lower nozzle temperature often gives cleaner details and less stringing.
→ Strongest parts
A higher layer height and temperature along with less layer cooling make the layers bond harder. You compromise a little on surface finish but get tougher, stronger parts.
Frequently asked questions about printing PETG
What temperature should I print PETG at?
According to our data sheets, 220–255 °C for the nozzle and 50–70 °C for the bed. A good starting point is around 235 °C for the nozzle and 60 °C for the bed, then you fine-tune with a temp tower.
Why do I get stringing with PETG?
Most often because of too high a temperature or damp filament. Lower the nozzle temperature in steps of 5 °C, make sure the filament is dry, and tune the retraction distance and speed.
Do I have to dry PETG before printing?
Not always, but PETG absorbs moisture from the air and damp filament gives poorer results. Store it dry with desiccant, and dry it if you see signs of moisture such as stringing or brittle parts.
Does PETG need a heated bed?
Yes, a bed temperature of around 50–70 °C is recommended for good adhesion. PETG adheres well to most build plates, and for large parts glue stick or a PEI plate can help.
PETG in 34+ shades, from 113 SEK
Every colour test-printed, vacuum-packed with a silica gel sachet and shipped from Tibro within 48 hours.